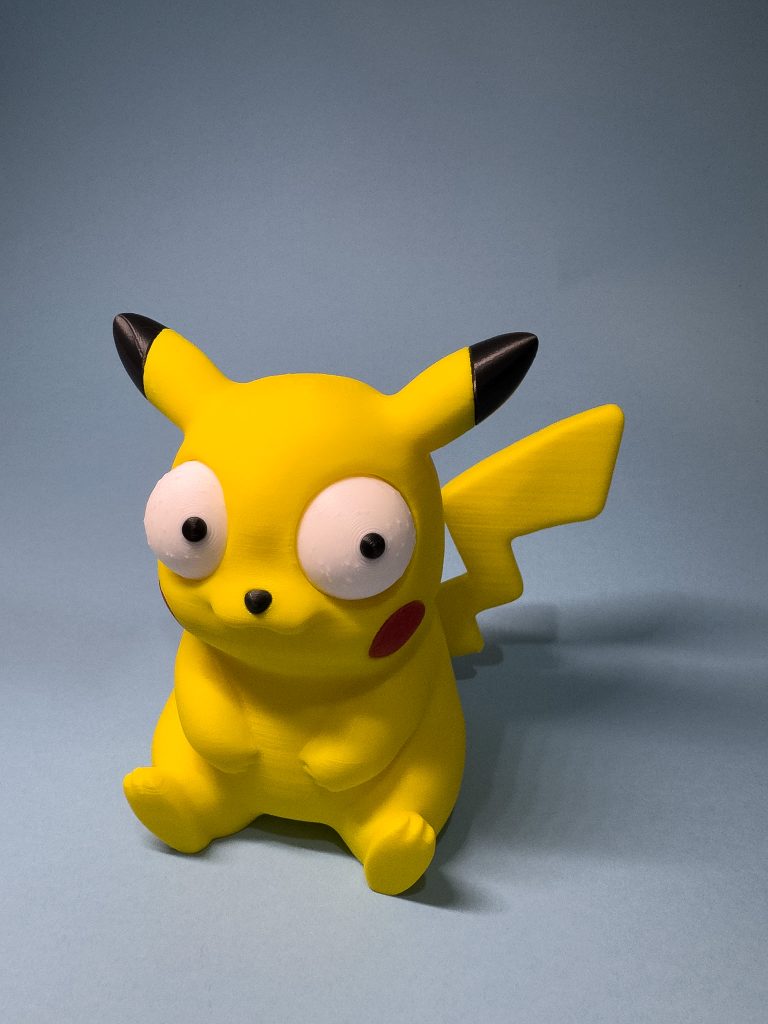
Luckily, I have finally managed to complete the print I started a few days ago. I ended up starting all over again and with a new 1kg pool of yellow filament, printed Pikachu without a hitch.
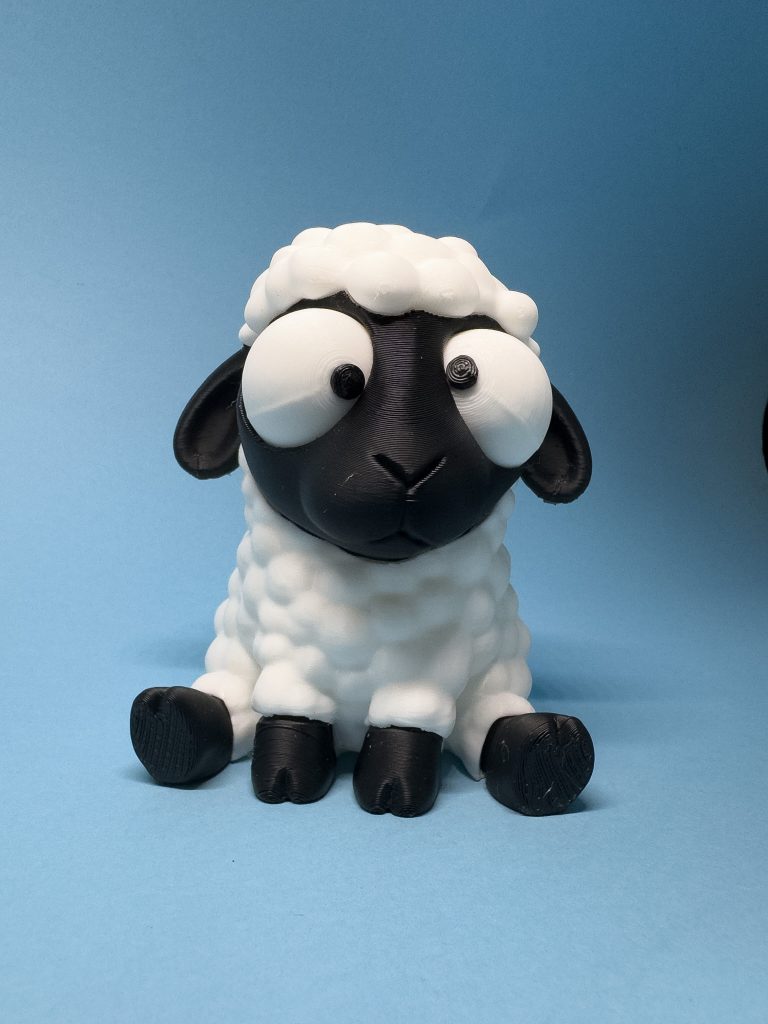
Confident that all was well with the printer, for an encore, I printed a sheep in a similar style to the Pokemon character, complete with moving eyes.
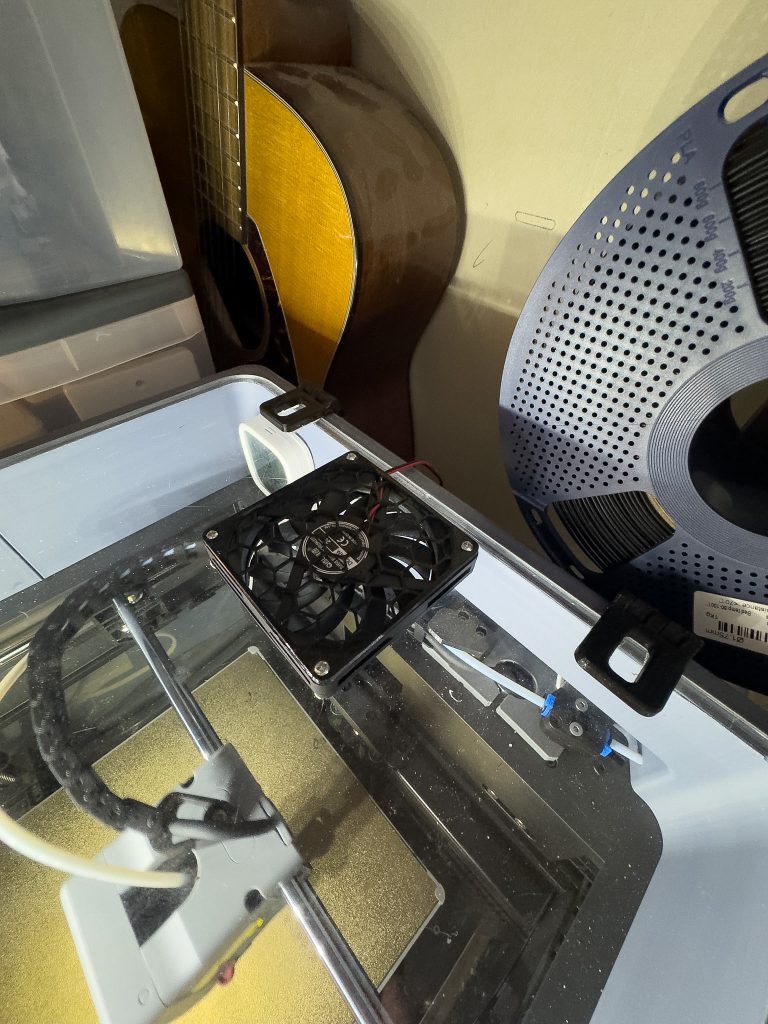
Happy with the cooling fan that I installed in my Flashforge AD5X (which I call YELLOW on account of it’s yellow enclosure) I have done a similar thing to my (slightly) older BLACK printer.
The enclosure for the Black printer is not a high as Yellow so I’ve had to mount the fan into the lid.
Whereas the fan on Yellow is controlled, manually, with a switch on the front of the unit, I can control the Black fan via software.
Feeling clever, I have added commands to the slicer software to automatically turn on the fan when printing PLA to prevent the dreaded heat creep.
However, when printing PET-G I can leave this fan off as that material copes better with higher temperatures.
When printing with the potentially challenging ABS, I need to keep the air in the enclosure around 45 – 50 degrees so the extract fan stays off but another fan which recirculates the air runs instead.
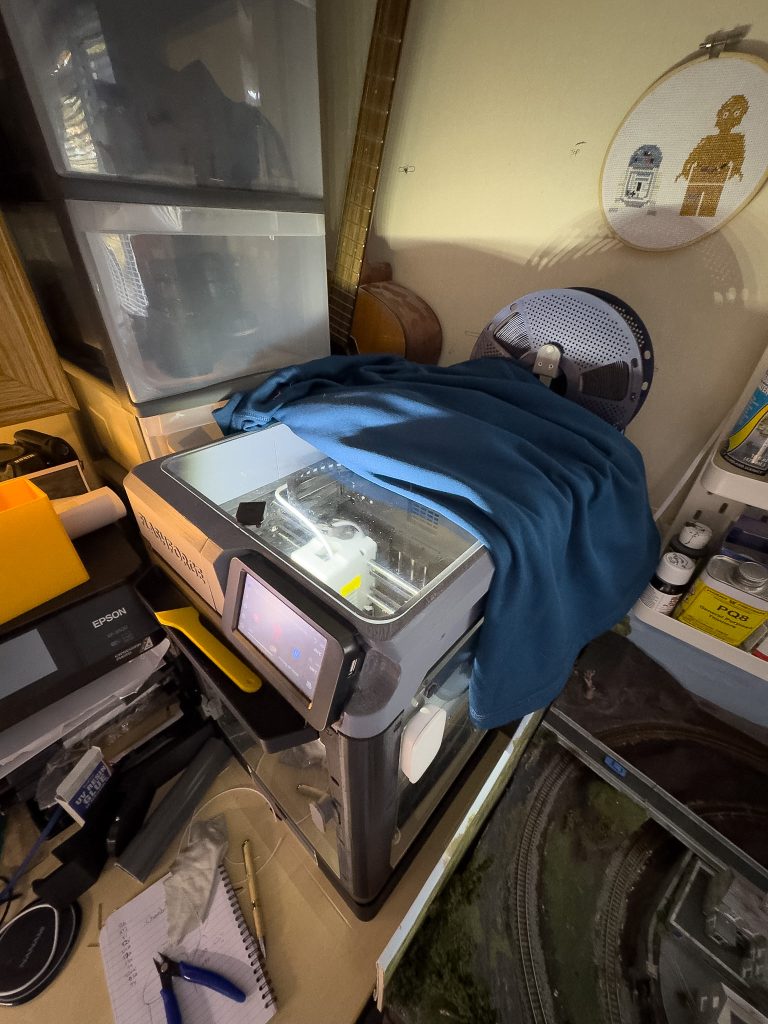
To assist in keeping the chamber temperature up high when printing ABS I have covered the machine, in this case with a fleece, to block the exhaust fan and insulate the machine.
I have done a few more long (six hour plus) PLA prints with the extract fans running without any problems so I may have cracked this 3D printing lark.